

CBM & Geothermal Drilling Mud Recycling Solutions
Optimize Drilling Fluid Performance in CBM and Geothermal Operations
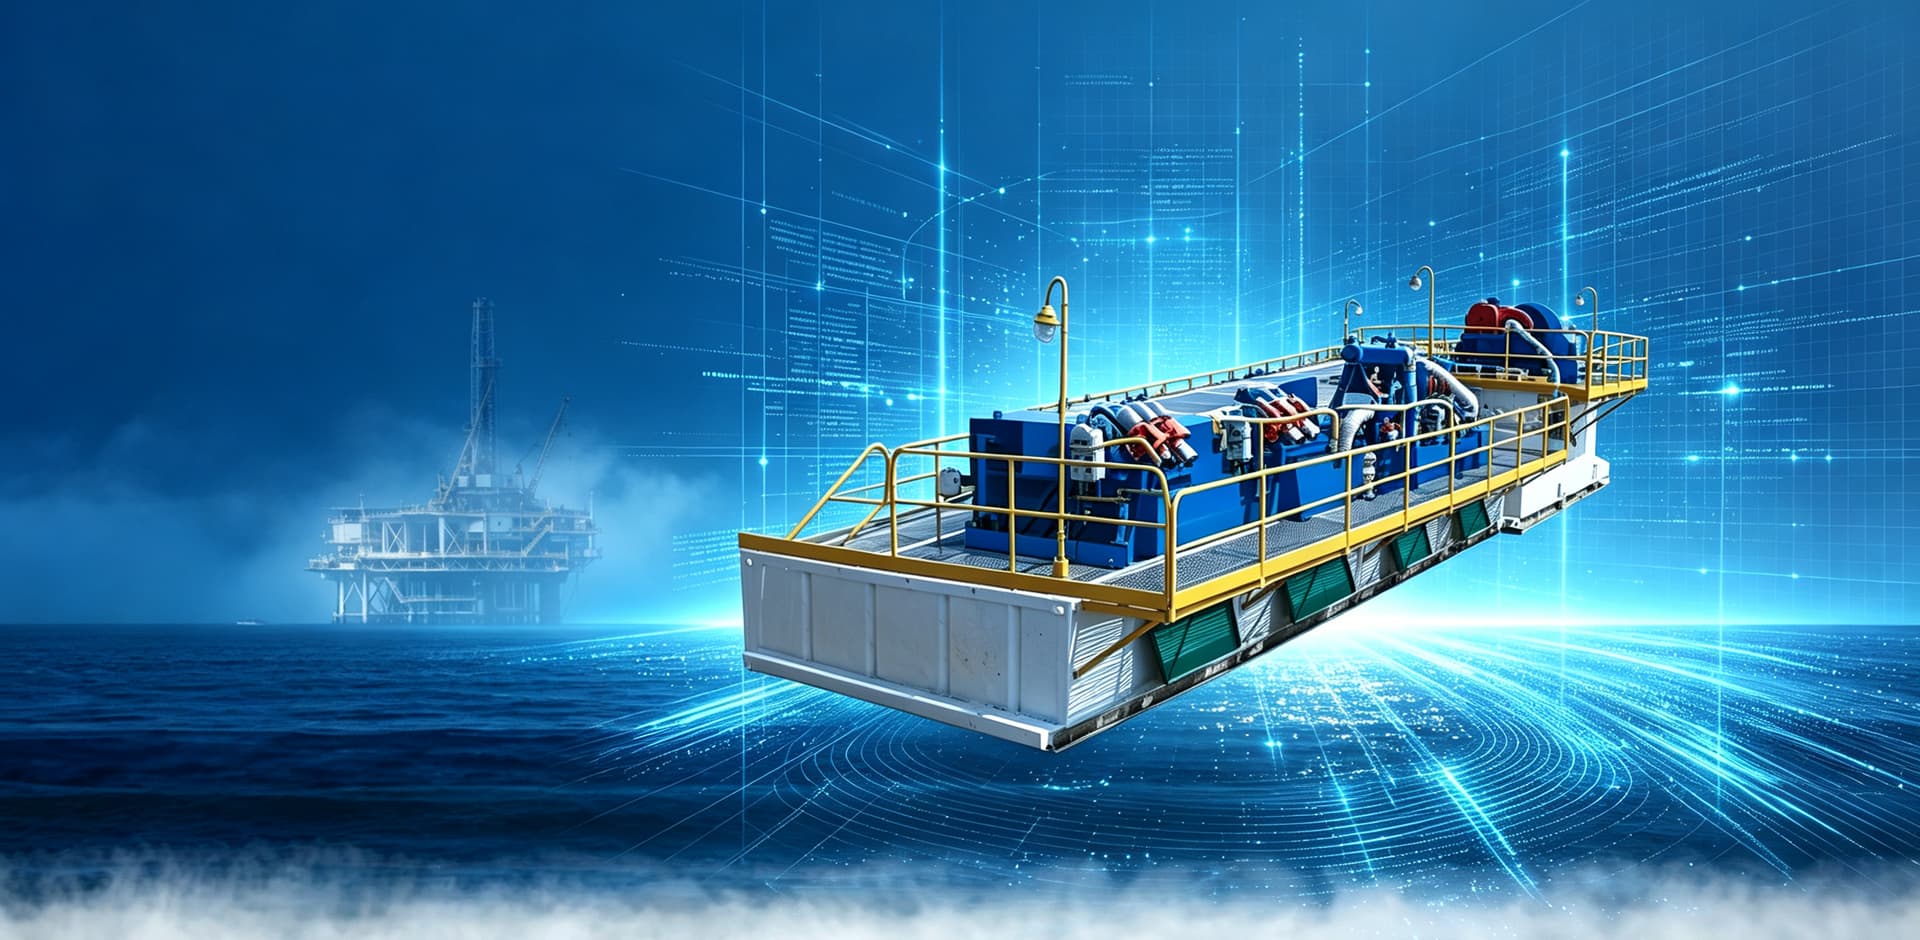
CBM & Geothermal Drilling Mud Recycling System
Challenge
Complex Drilling Conditions and Demanding Mud Management Requirements
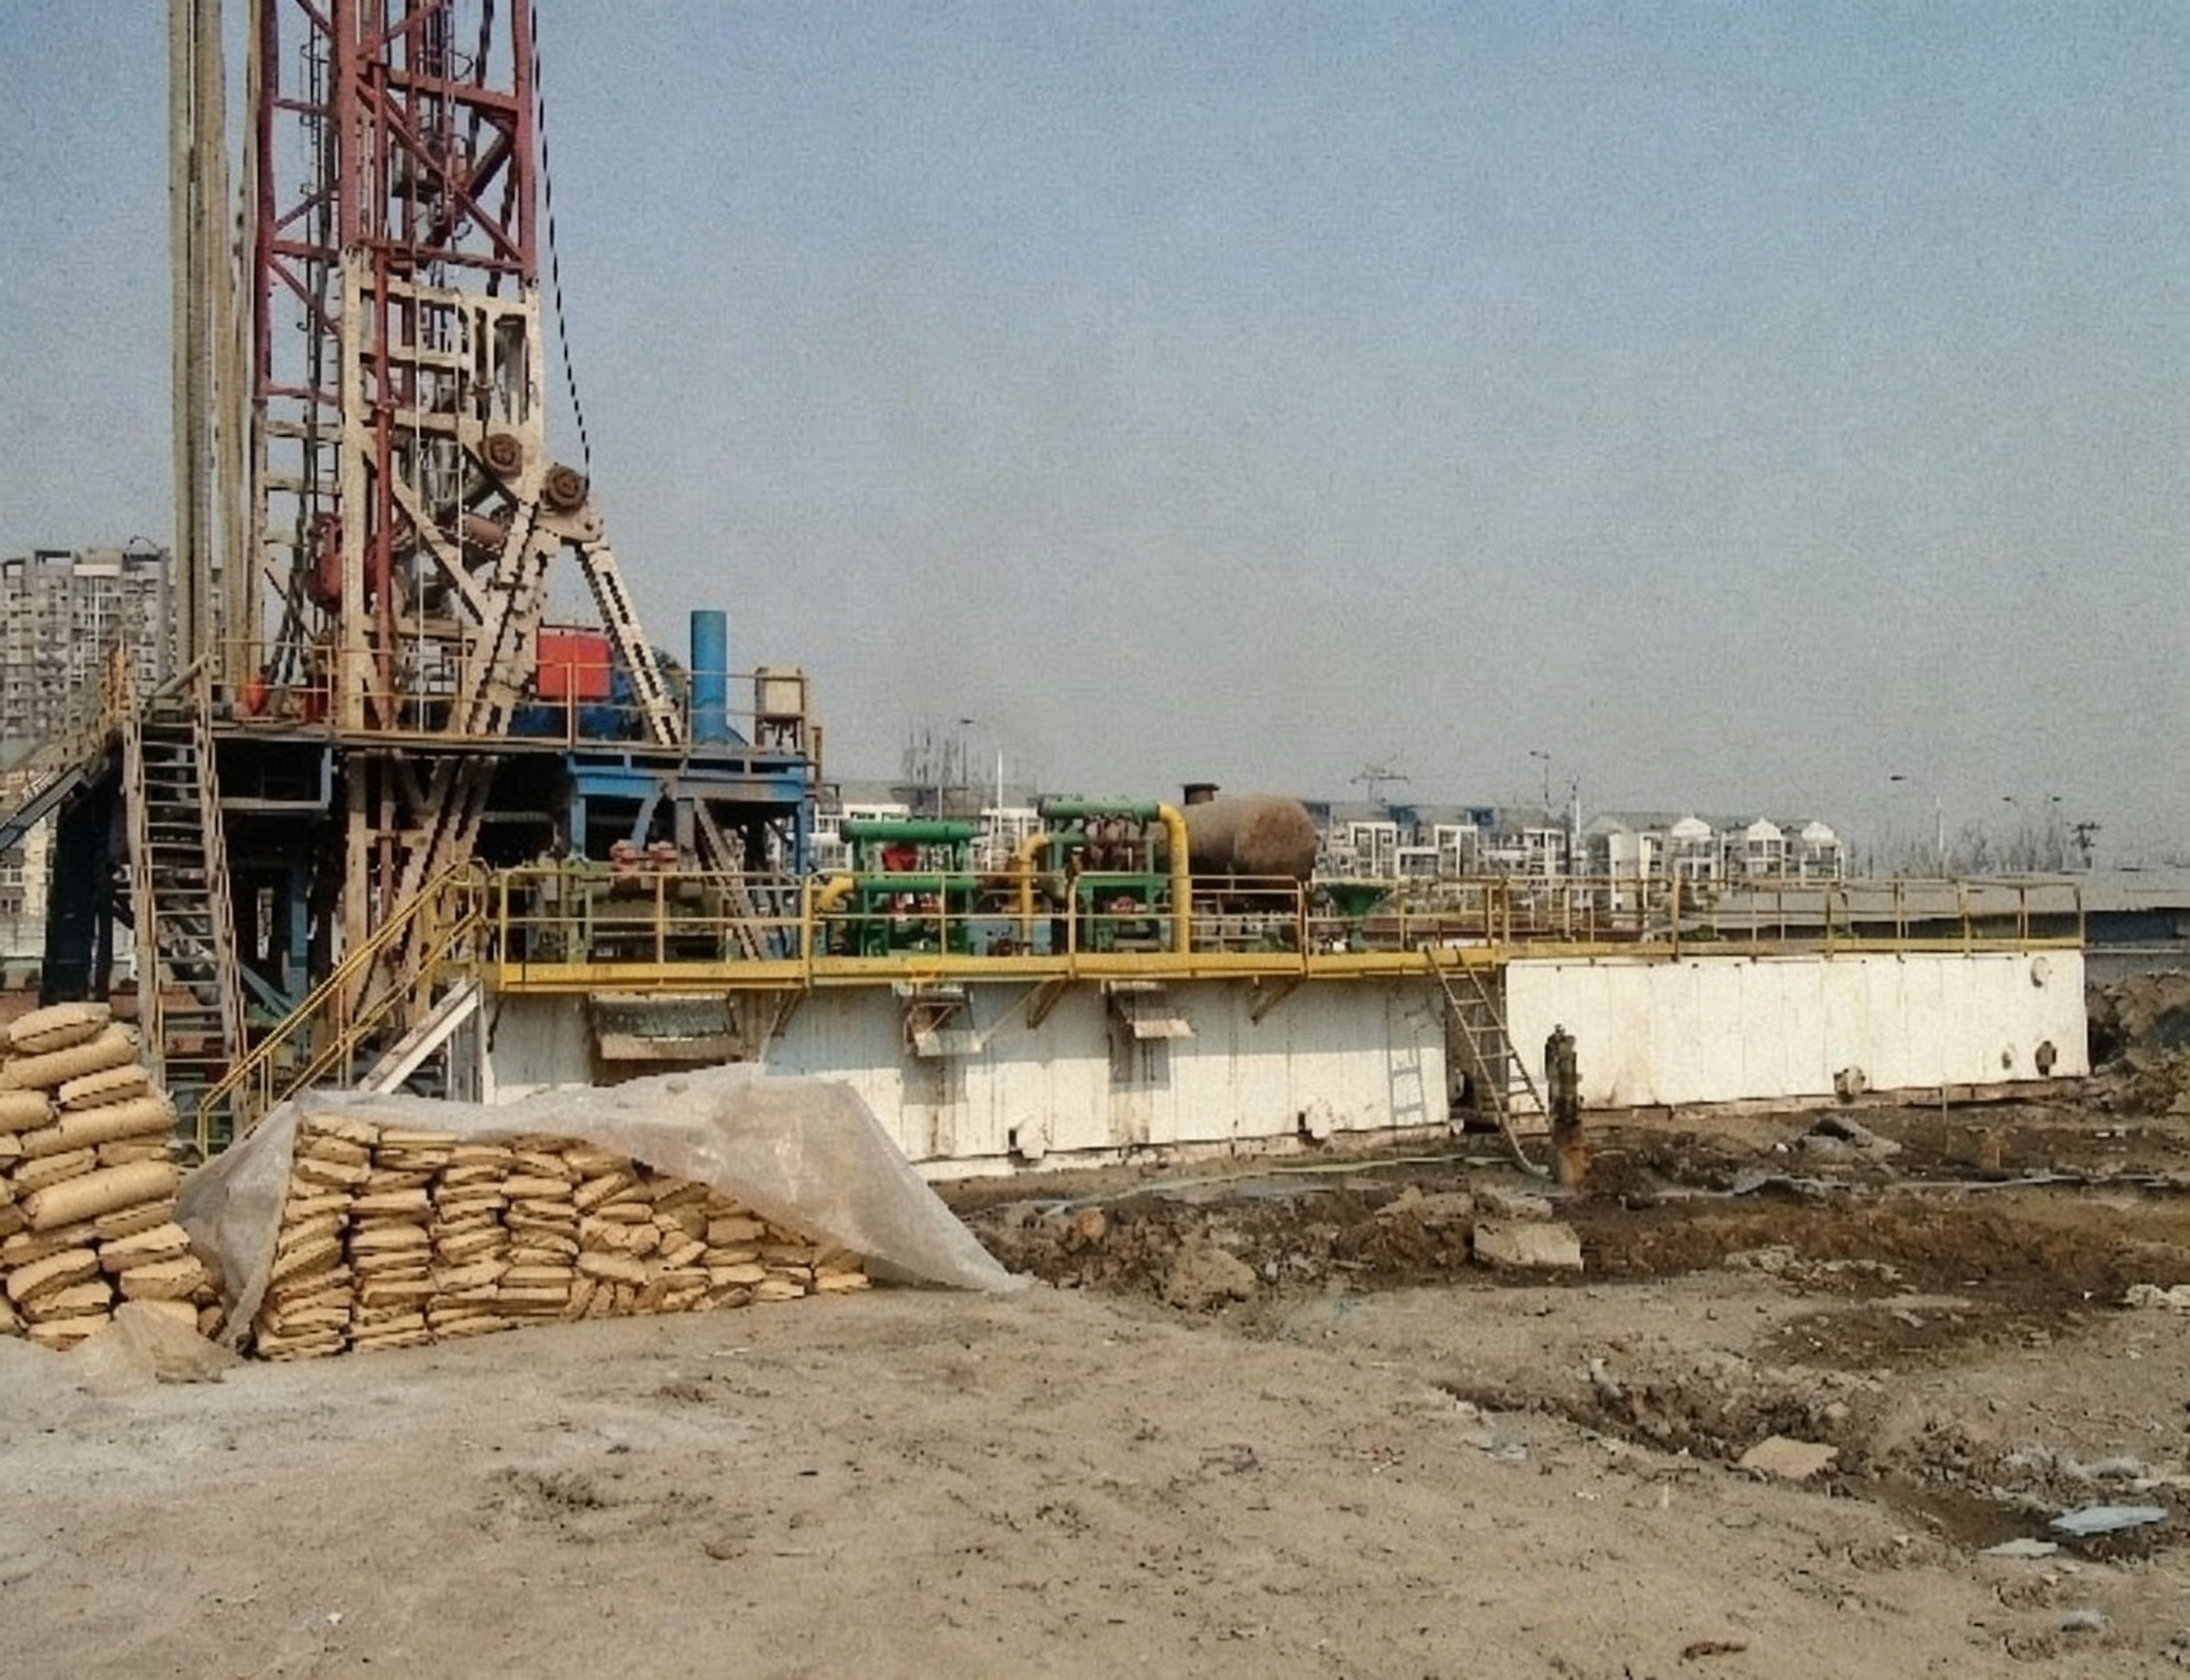
Coalbed Methane (CBM) and Geothermal drilling present unique challenges, including fine coal particles, high temperatures, hard rock formations, gas influx, and strict environmental requirements. Continuous mud recycling is critical to maintaining fluid properties, ensuring wellbore stability, reducing costs, and minimizing environmental impact.
Solutions
Advanced Mud Recycling System for CBM & Geothermal Drilling Applications
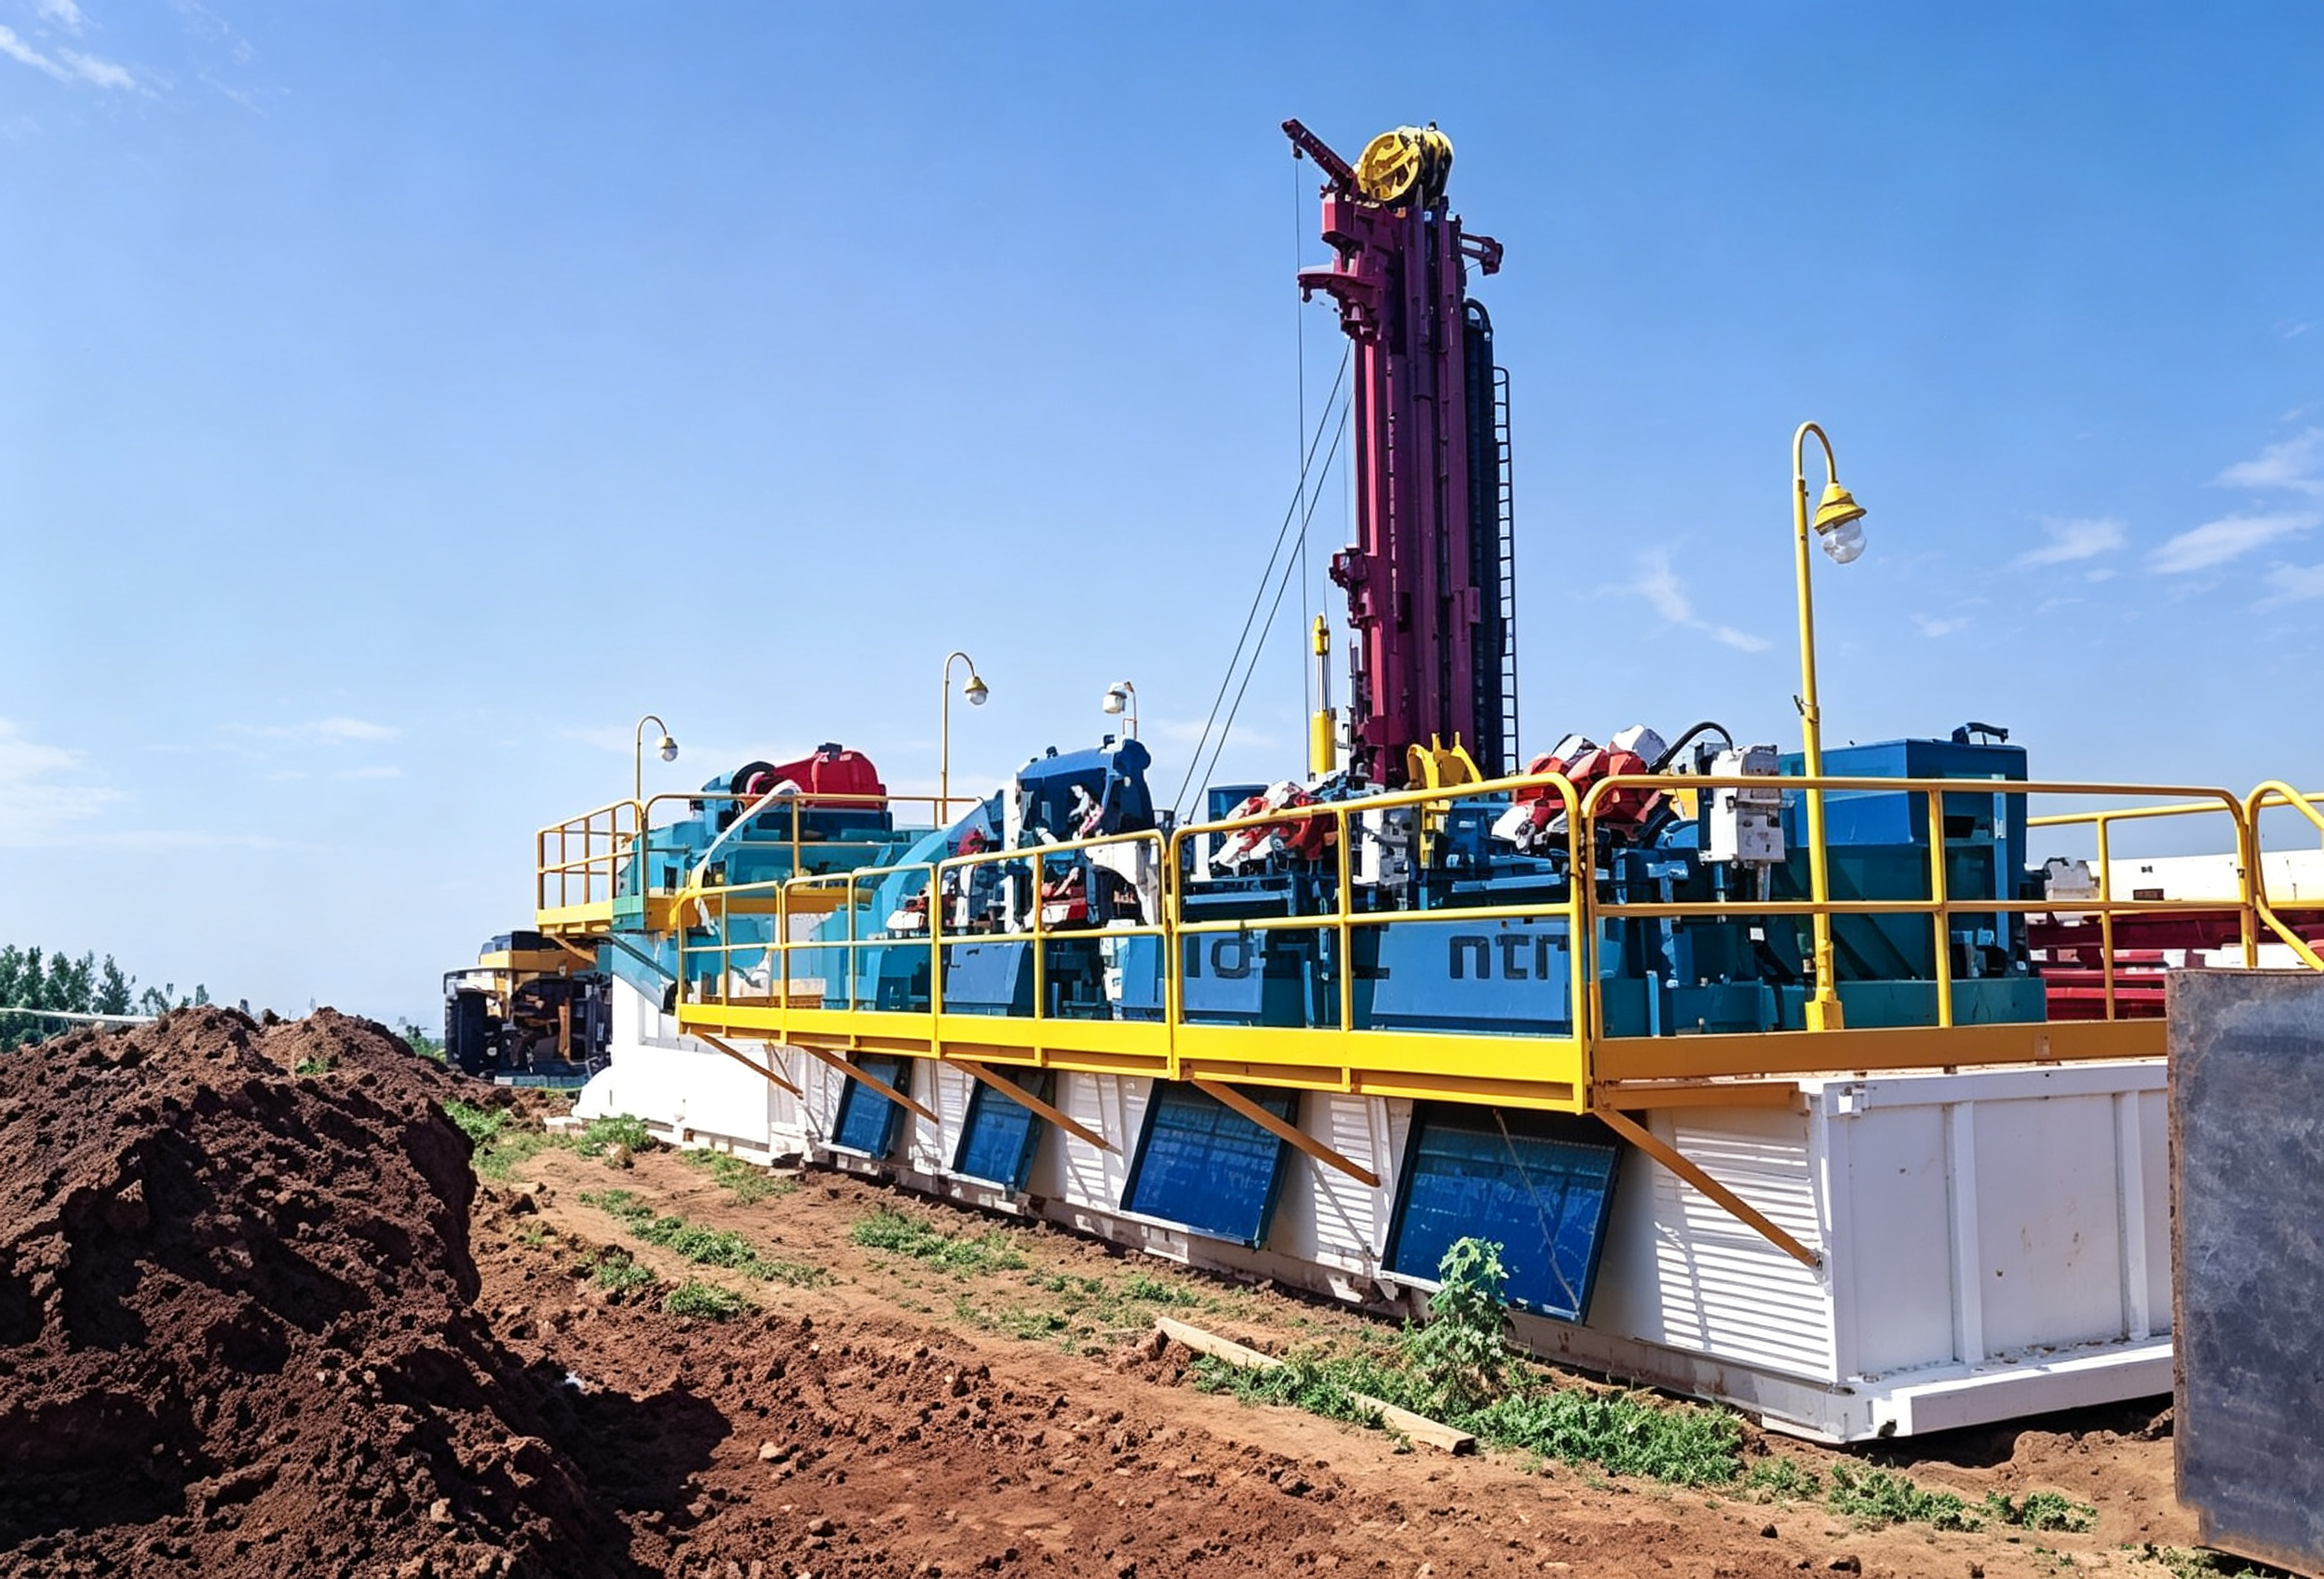
Our CBM & Geothermal Drilling Mud Recycling System provides high-efficiency solids control and fluid recovery tailored for these demanding applications, helping maintain optimal drilling fluid performance while supporting stable, cost-effective, and environmentally responsible operations.
Components
Core Equipment for CBM & Geothermal Drilling Mud Recycling System
A full set of CBM and geothermal mud purification system adopts multi-stage graded separation and supporting conditioning equipment to precisely control solid content, adjust mud performance and realize closed-loop mud recycling.
Drilling Fluid Graded Separation Equipment
Mud Circulation & Delivery Pumps
Mud Conditioning & Mixing Equipment
Mud Tank Assembly
Multi-stage separation units to remove coarse, medium and ultra-fine drill cuttings from return mud

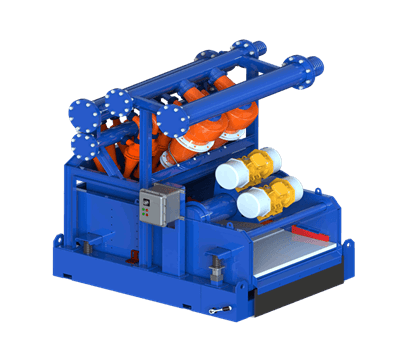
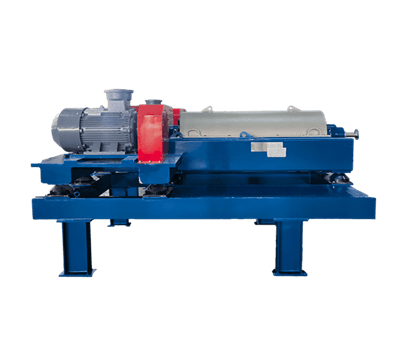
Provide stable power for mud feeding and full-system circulation


Stabilize mud properties and prevent solid sedimentation inside tanks


Complete tank group for mud sedimentation and blending

Highlights
Integrated CBM & Geothermal Drilling Mud Recycling Solutions
Our solution highlights its core capabilities and the real, measurable value it delivers.

Multi-Stage Solids Control
Linear motion shale shakers for initial coarse removal, followed by desanders, desilters, and mud cleaners for particles down to 15-20 microns.
High-Speed Decanter Centrifuges
Excellent removal of ultra-fine solids common in coal seams and hard geothermal formations.
Gas Separation & Degassing
Liquid-gas separators and vacuum degassers to safely handle methane and other gases in CBM drilling.
High-Temperature Compatible Components
Robust equipment designed for elevated temperatures and aggressive fluids typical in geothermal wells.
Compact Modular Design
Skid-mounted or trailer-mounted systems with partitioned tanks, agitators, and mixing hoppers for easy transport and fast rig-up.
Automation & Real-Time Monitoring
Density, viscosity, sand content, and flow monitoring with optional PLC control for consistent performance.
Major Cost Savings
Recycle drilling fluid effectively, reducing consumption of bentonite, polymers, and water by 50-70% while lowering disposal and transportation costs.
Enhanced Drilling Efficiency
Maintain optimal mud properties for better hole cleaning, wellbore stability, and higher penetration rates in challenging coal and hard-rock formations.
Improved Safety
Effective gas handling in CBM operations and reduced risk of lost circulation or stuck pipe in geothermal wells.
Environmental Compliance
Minimize waste volume, reduce site footprint, and support closed-loop or near-zero discharge operations.
Extended Equipment Life
Cleaner fluid decreases wear on pumps, bits, and downhole tools, especially important in abrasive geothermal conditions.
Why Choose Our CBM & Geothermal Mud Recycling System?
- Specifically engineered for the unique demands of CBM (fine coal solids & gas) and Geothermal (high temperature & hard formations) drilling.
- Rugged, reliable design with proven performance in coalbed methane fields and high-temperature geothermal projects worldwide.
- Customizable configurations to match your rig specifications and site constraints.
- Comprehensive support from system design through commissioning and ongoing maintenance.
Case Studies
Proven Solutions, Real-World Results
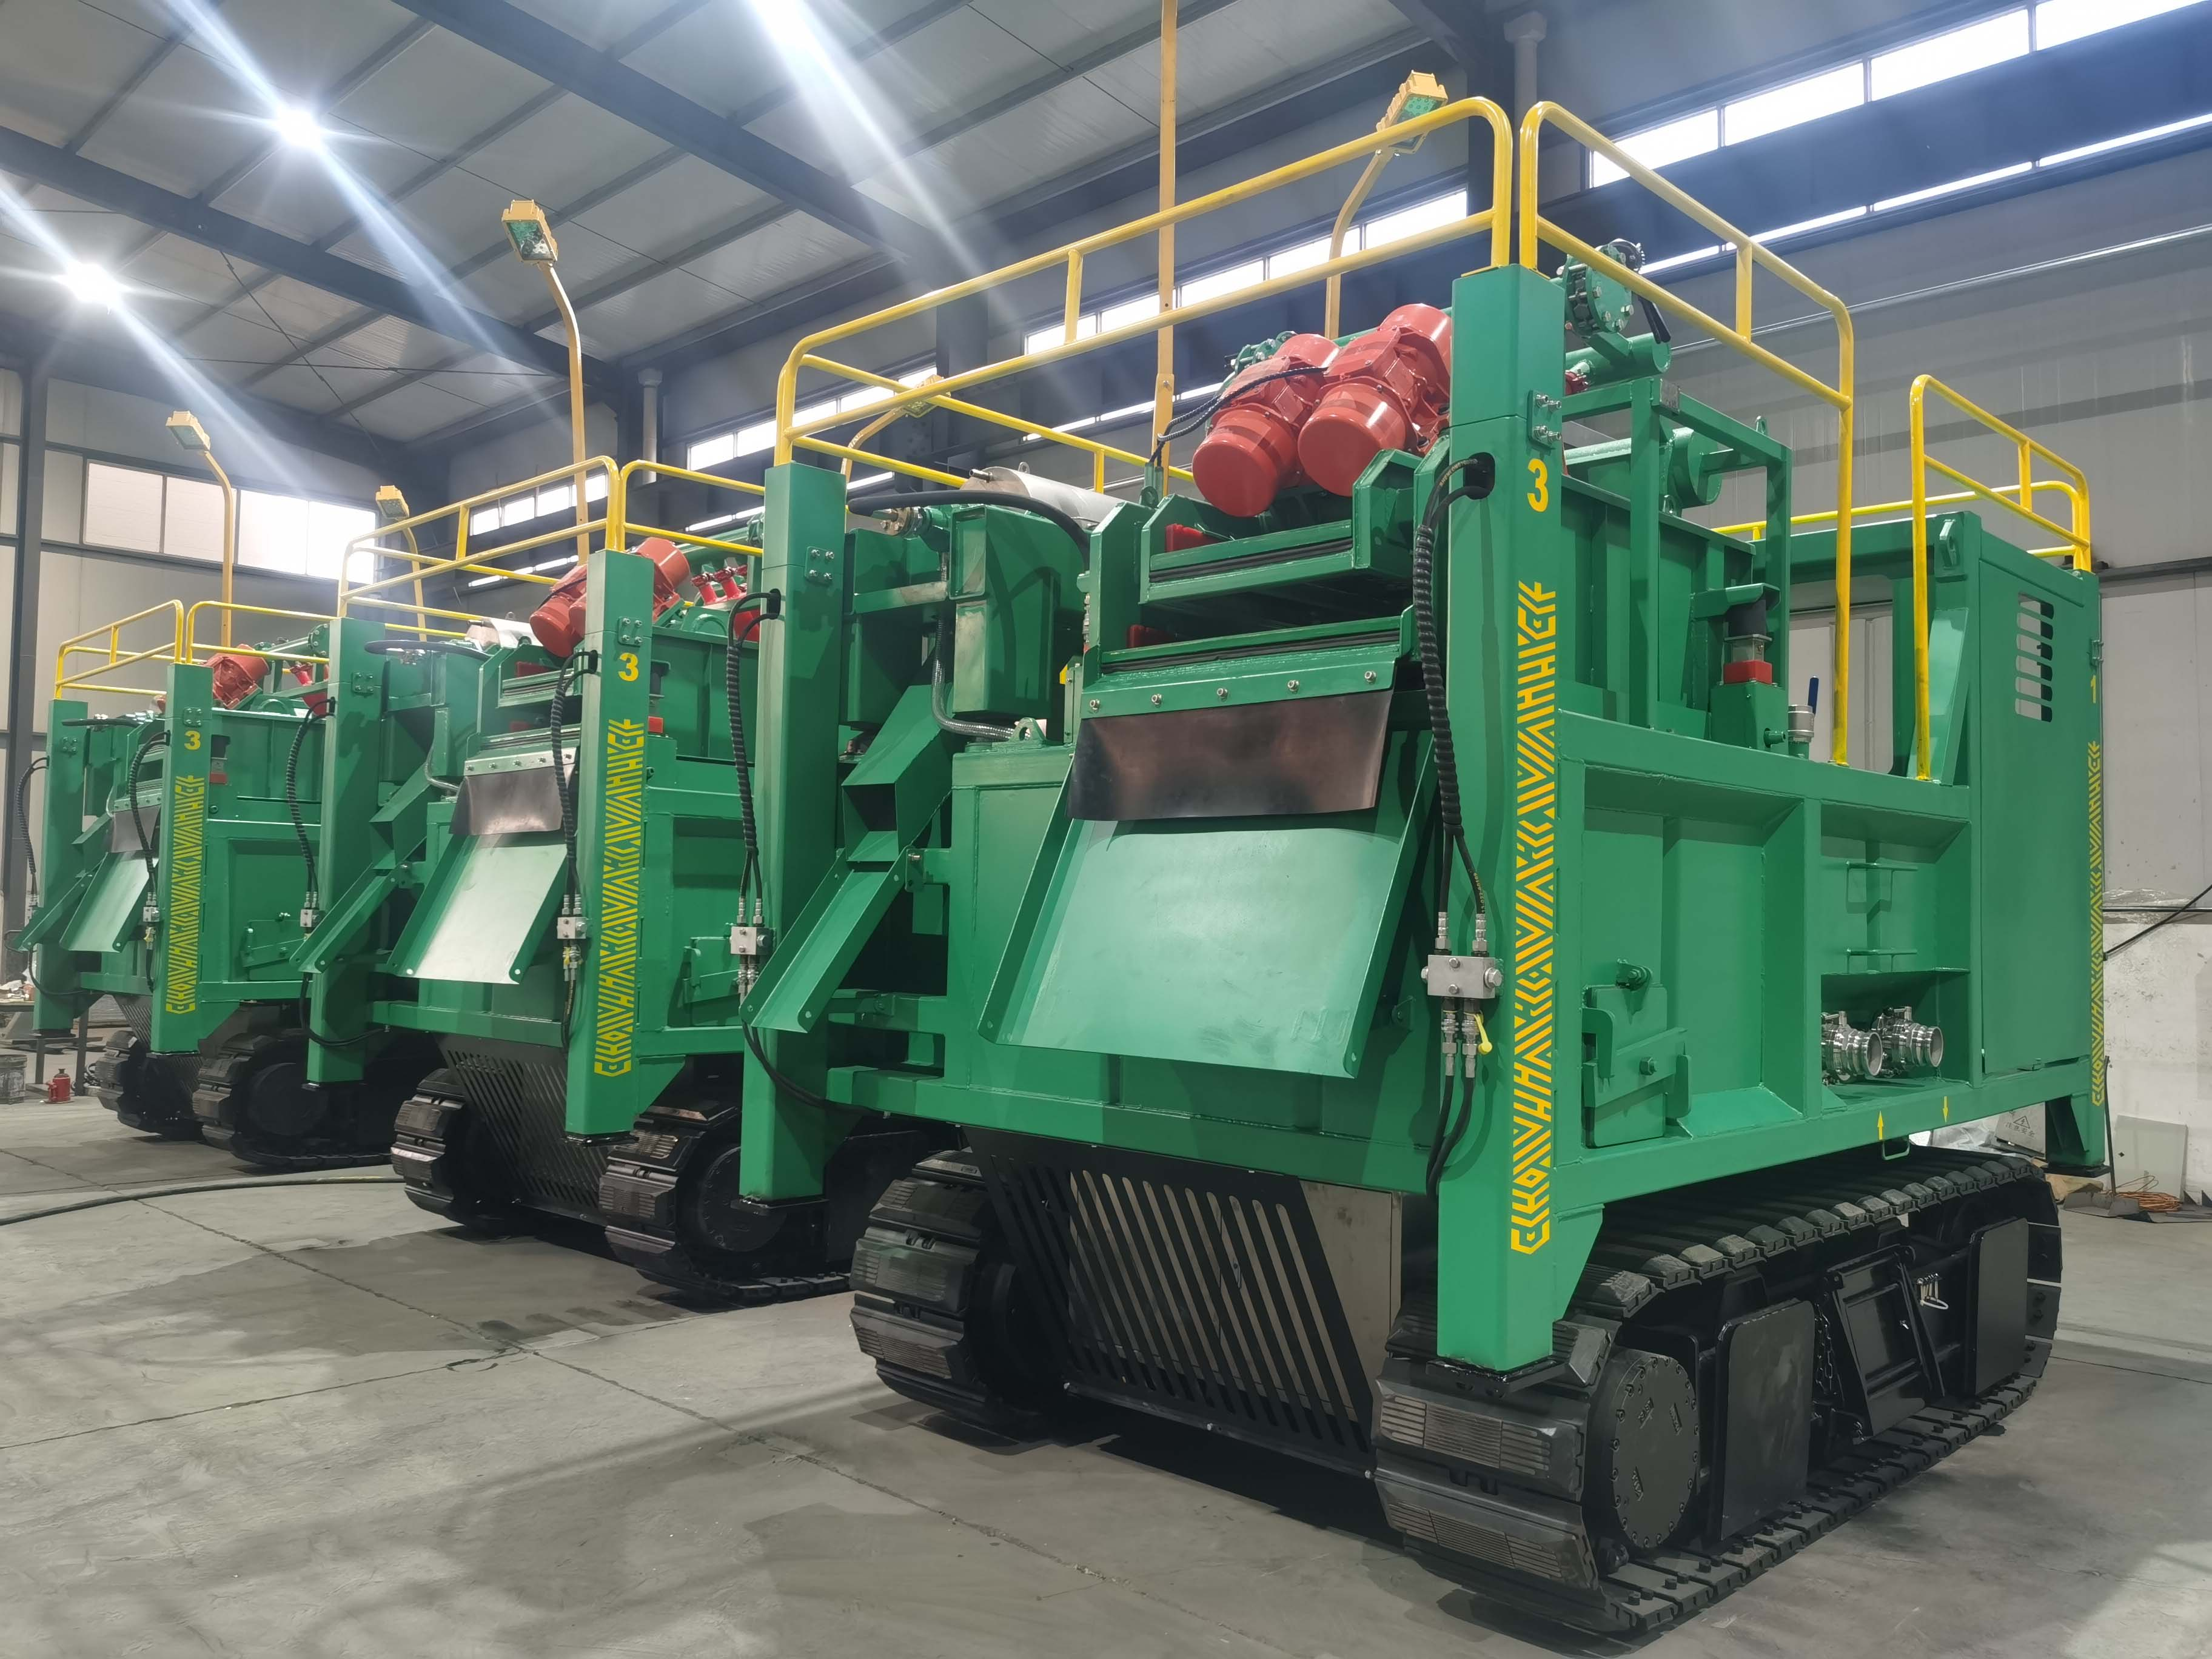
Truck-Mounted Mud Recycling System Project (United Kingdom)
Challenge
Frequent site relocation, strict UK waste discharge rules & high slurry hauling expenses.
Solution
Mobile skid truck-mounted multi-stage solids control system for full on-site mud closed-loop recovery.
Frequent site relocation, strict UK waste discharge rules & high slurry hauling expenses.
Solution
Mobile skid truck-mounted multi-stage solids control system for full on-site mud closed-loop recovery.
Field Feedback
“
Reliability is critical for our desert drilling operations. Henyo’s equipment has been running continuously under harsh field conditions for more than a year, and the performance has been very stable. We have experienced very few maintenance issues with the mud cleaner, and the overall build quality has met our expectations. When we needed spare parts for the pump, the service team responded quickly and helped us minimize downtime. Based on our experience, Henyo has become a trusted partner for our future drilling projects.
Mohammed Al-Hassan
Drilling Operations Manager
“
We have evaluated several brands of solids control equipment over the past two years, and Henyo’s shale shaker and decanter centrifuge have delivered the most consistent performance. The equipment handles high-volume drilling operations smoothly and performs beyond our initial expectations. What impressed us most is the efficient fluid recovery, which helped us reduce drilling fluid consumption during this project. The cuttings discharge is also noticeably drier, making waste handling easier and helping us meet environmental requirements without issues.

John Miller
Procurement Manager
“
Before switching to Henyo’s integrated solids control system, we were using equipment from different suppliers, which created many compatibility issues. The shaker, cascade system, and centrifuge now work together smoothly as one complete solution. The centralized control system makes daily monitoring much easier for our team, and the centrifuge has maintained good performance after multiple wells. Henyo’s integrated approach has helped us improve operational efficiency and better control drilling fluid costs.”
Robert Williams
Project Manager
CBM & Geothermal Drilling Mud Recycling System FAQs
What is a CBM & Geothermal drilling mud recycling system used for?
The system is designed to continuously process and recycle drilling fluids in Coalbed Methane (CBM) and Geothermal operations. It removes drilled solids, fine coal particles, and entrained gas while maintaining stable mud properties to support efficient drilling performance, wellbore stability, and reduced environmental impact.
What level of solids control efficiency can the system achieve?
The integrated multi-stage solids control package—shale shakers, desanders, desilters, and mud cleaners—can efficiently remove solids down to 15–20 microns. For ultra-fine particles common in CBM and geothermal formations, high-speed decanter centrifuges provide further separation to maintain optimal mud quality.
How does the system handle gas influx in CBM drilling?
The system is equipped with vacuum degassers and liquid-gas separators specifically engineered to safely remove entrained methane and other formation gases from drilling fluids. This helps reduce well-control risks, improve safety, and maintain consistent mud density and performance.
Can the system operate under high-temperature geothermal conditions?
Yes. All critical components are designed with high-temperature-resistant materials and robust structural configurations. Agitators, tanks, sensors, and separation equipment are engineered to maintain stable performance under harsh geothermal drilling environments.
What are the typical capacity ranges available?
The system is modular and scalable, with standard configurations ranging from 200 GPM to 1500+ GPM. Capacity can be customized based on rig size, well depth, formation characteristics, and project requirements.
What operational and economic benefits does the system provide?
Operators typically achieve significant reductions in drilling fluid consumption (up to 50–70%), lower waste handling costs, improved rate of penetration, and enhanced equipment lifespan. The closed-loop recycling process also supports stricter environmental compliance and reduces overall site footprint.
Let’s build a sustainable oilfield future together!
Whether developing a new drilling project or enhancing an existing solids control system, Henyo Petro delivers proven equipment, engineering expertise, and integrated solutions that help improve drilling efficiency, maximize fluid recovery, and reduce waste.


